Bowl liners and mantles cast in high manganese steel with TiC-insert alloy bars through the wear zone — for standard and short-head cone crushers.
A cone crusher reduces rock by squeezing it between two wear surfaces inside the crushing chamber:
Rock enters at the top and is crushed progressively as it travels down the cavity. The gap between the two liners at the bottom is the closed-side setting (CSS), and that setting is what fixes your product size.
Both liners are consumables. In hard abrasive rock they are the parts you change most often — and every change means the crusher stops, the circuit stops and the crane comes out.
A normal set consists of a bowl liner or concave (often split into upper, middle and lower rings), a mantle, and the fittings: torch ring, locking nut, epoxy backing and feed cone.
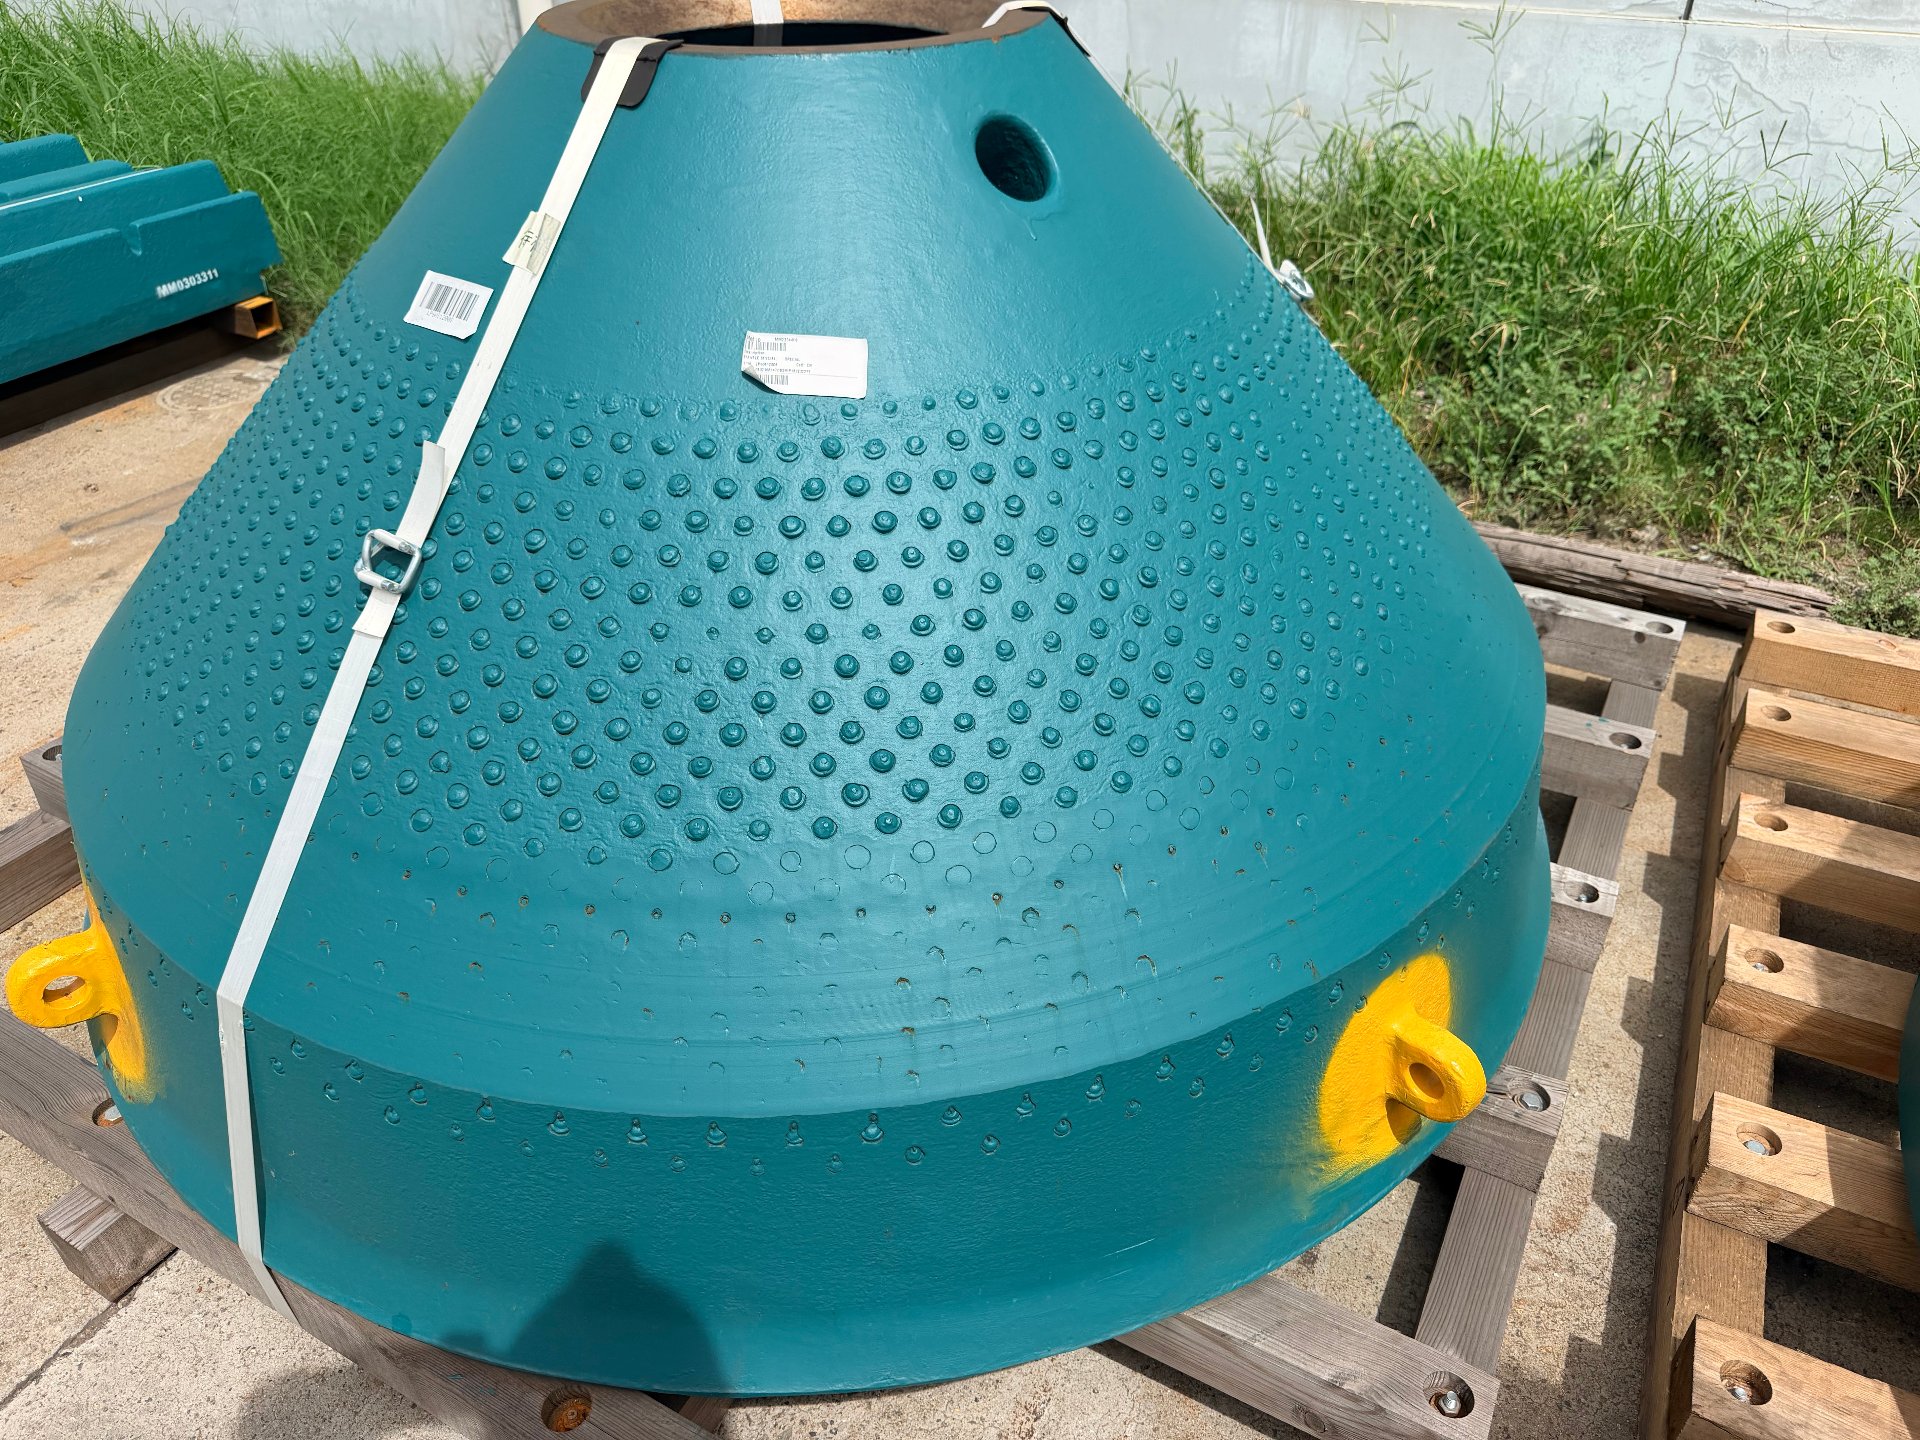
A cone liner does not wear evenly. Each band of the chamber does a different job and fails in a different way, which is why the insert layout is set zone by zone rather than as one grid.
Coarse rock arriving at speed. Impact-dominated — the surface peens and the metal flows before it ever wears smooth.
Sliding abrasion under load. This is where the profile starts to open and the chamber volume changes.
The punishing band — high pressure, tight clearance, rock held and ground. Service life is decided here.
Controls the setting. Wear here moves your CSS and the size split of the product directly.
An insert pattern that is dense in the parallel zone and open at the feed end costs the same to cast as a uniform one — but it wears where the chamber actually wears.
A cone liner is cheap to buy and expensive to run. These are the six costs that show up on the balance sheet.
A liner change is 8–24 hours of lost production plus crane time and labour. In abrasive granite or basalt duty a plain manganese liner can be finished in weeks, not months.
As the liners wear the cavity opens. Reduction ratio drops, the product curve shifts, fines and oversize both creep up, and the power draw moves away from what the plant was designed around.
The feed end, upper chamber, parallel zone and discharge end all wear at different rates. One band is often scrap while the rest of the liner still has life — but the liner comes off as one piece.
Cone liners are heavy. Holding a full set of spares ties up cash and floor space, and air-freighting an emergency liner costs more than the liner.
When the life of a liner varies between batches, planning a maintenance window becomes guesswork — and you carry extra stock just to cover the variance.
A low purchase price means more change-outs per year. The number that decides your maintenance budget is cost per tonne crushed, not cost per part.
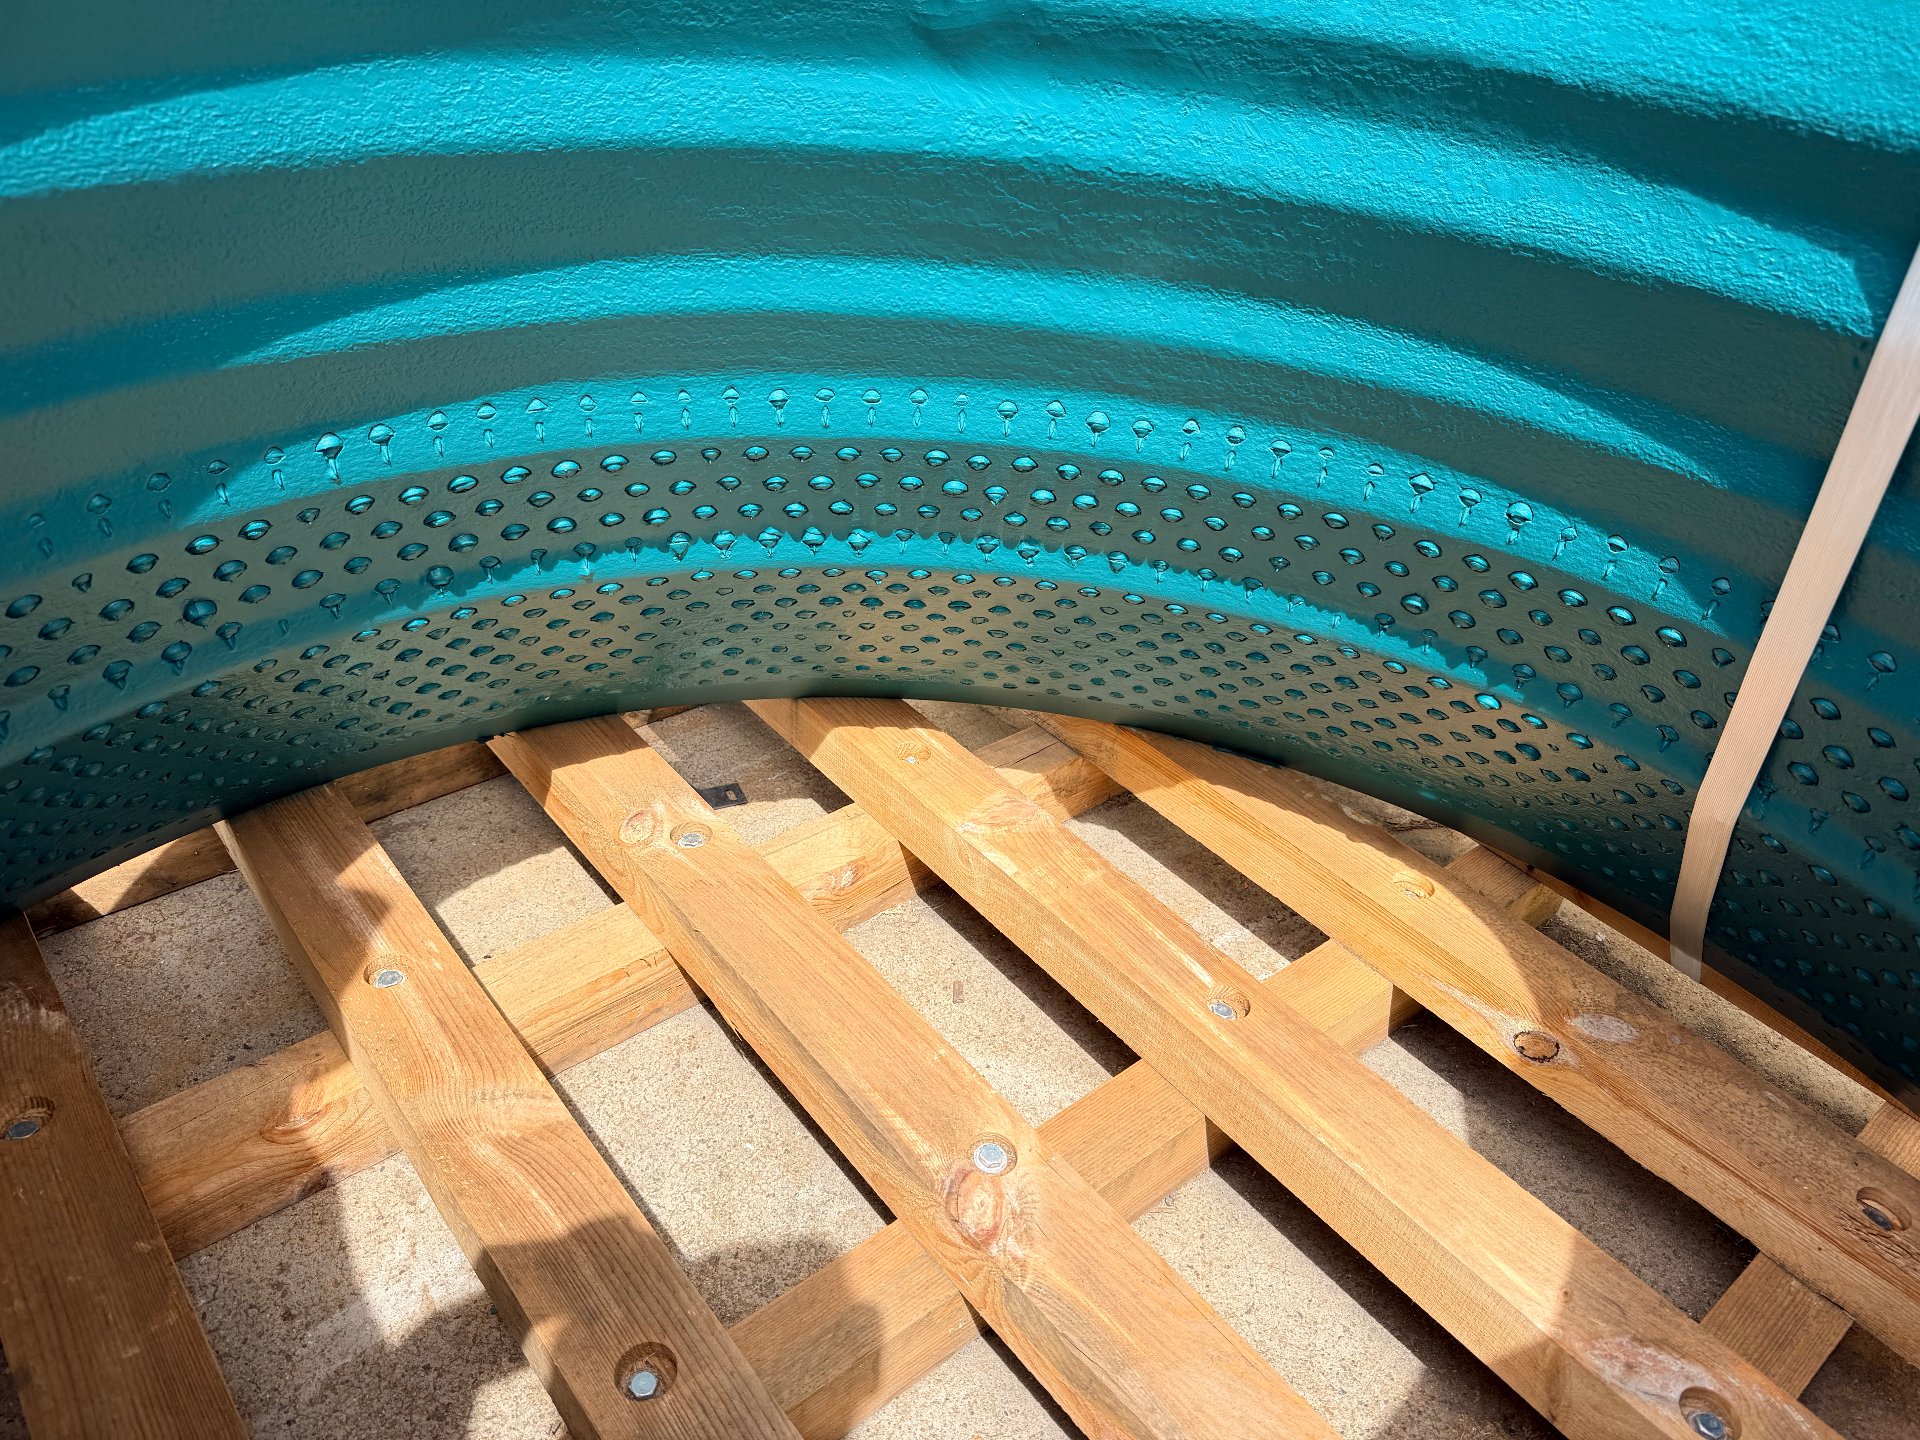
Cost per campaign: a composite liner costs about 1.4× a plain manganese casting and returns roughly 2× the wear life. Against a carbide-bar composite of the same layout it lands at about 75% of the price, with performance in the same class.
| Item | Typical carbide bar composite | CA-Alloy 60 composite |
|---|---|---|
| Wear bar layout | Same pattern | Same pattern |
| Relative price, same layout | 100 | ≈ 75 |
| Hardness (wear bars) | 60–62 HRC | 58–61 HRC |
| Bending strength | ≈ 1900 MPa | 1940 MPa |
| Impact toughness | ≈ 8.1 J/cm² | 9.0–12.0 J/cm² |
| Matrix | High manganese steel | High manganese steel |
Laboratory values for the wear alloy itself, not field-service guarantees. Relative price compares parts of the same layout and fitment; final pricing depends on part weight, cavity and quantity.
Gold ore, iron ore, and a West Australian mine running TP450 — all cone liners returned from service.
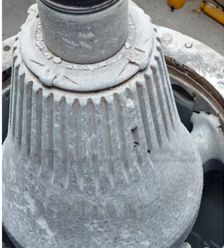
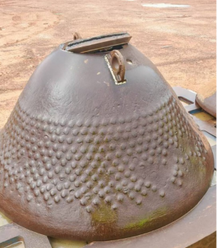
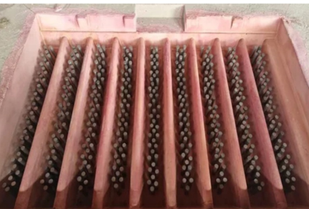
Bars are laid out to follow the wear pattern of each part — and because our bars come from our own plant, the layout runs far denser than a bought-in bar allows.
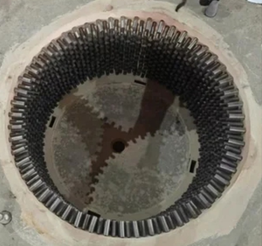
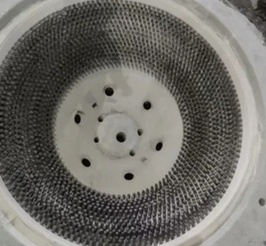
Parts returned from site service, same duty, two composite systems. Look at the insert sockets: one system loses them, the other keeps the face level.
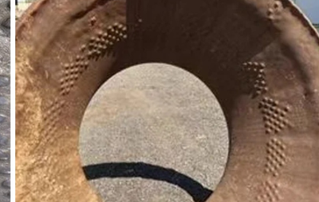
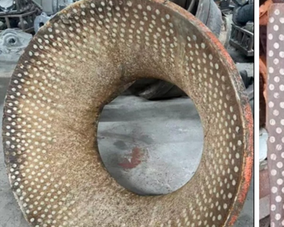
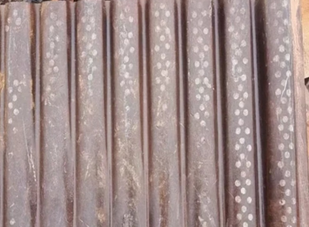
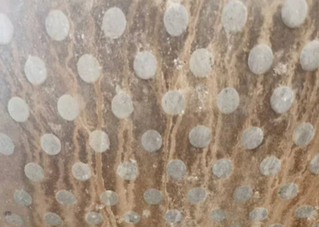
Standard and short-head cone crushers. These are the series we already tool patterns for — if yours is not listed, send the part number or a photo and we will confirm it.
Tell us the machine model and the part you are running now, and we will come back with the composite option measured against it.
A part number, a drawing, or simply a photo of the worn liner together with the machine model is enough for us to identify the fitment. You get a drawing back with the insert pattern marked before anything is cast.
How an order runs: confirm the part and the chamber configuration → map the wear zones → 3D-print the pattern and machine the mould → cast, heat-treat, machine and inspect → the set ships with batch records.
Send us your cone linerAll manufacturer names, part numbers, model numbers and descriptions are used for identification and reference purposes only. It is not implied that any part listed is the product of the original manufacturer. Wear performance figures are laboratory values for the wear alloy itself and are not field-service guarantees. Patented in China (CN106282835B).