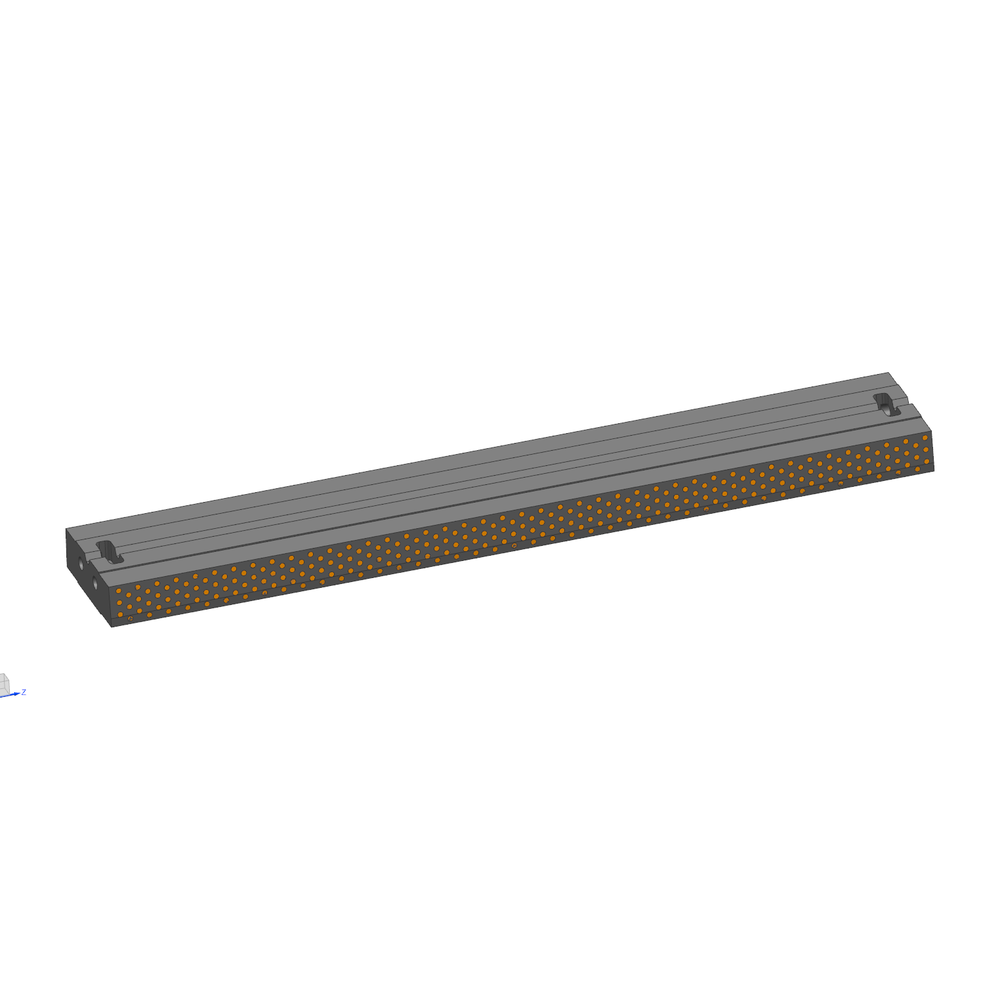
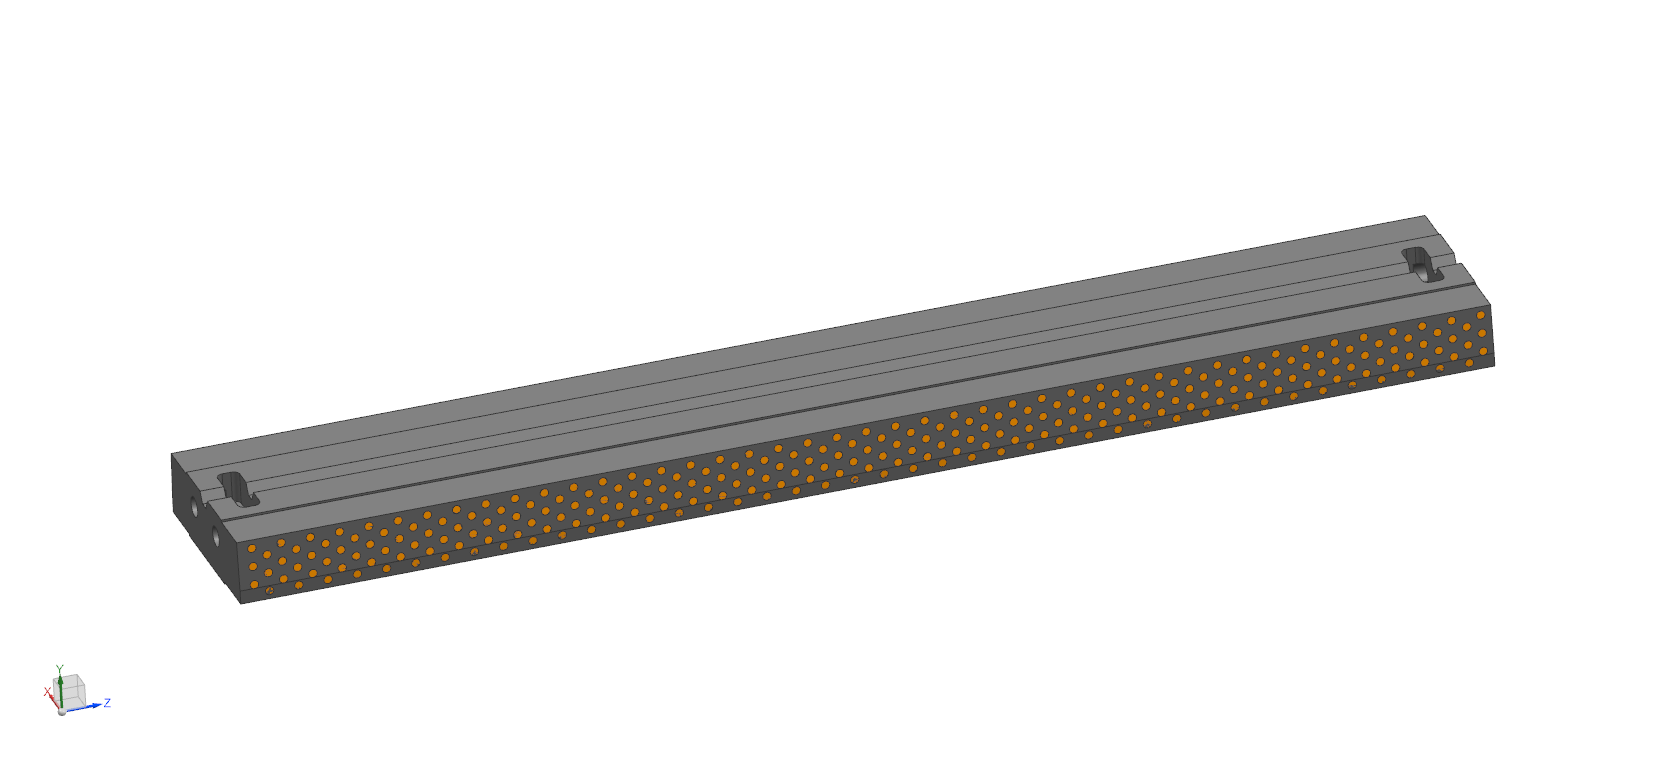
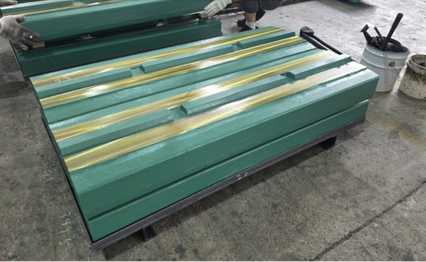
Impact blow bars cast in high manganese steel with TiC-insert alloy bars along the working edge — for horizontal shaft impactors.
A horizontal shaft impactor breaks rock by hitting it. The blow bars are the heavy bars mounted in the spinning rotor — four, six or eight of them depending on the machine — and they are the parts that actually strike the feed.
Material enters the chamber, is hit by the rotating bars, thrown against the impact plates and broken again on the rebound. A blow bar therefore works in a harsher regime than a compression liner: high-speed impact rather than slow squeezing.
When the leading edge wears back the bar is normally rotated to use its second face, then replaced. Two things end a blow bar’s life: abrasion of the working edge, and breakage when that edge chips or cracks.
A blow bar has two working faces. Whether the second one is usable is decided by the edge — not by the operator’s schedule.
The leading edge takes the hit. Abrasion rounds it off progressively — slow, predictable, plannable wear.
After rotation the other edge goes to work. This only exists if the first face wore out instead of breaking.
A bar whose edge chips loses half its life in a single event — and the operator finds out when the rotor comes out. That is the failure a cast-in composite bar with a tough austenitic matrix is built to avoid.
A blow bar is bought as metal and paid for by the tonne crushed. These are the six places that money leaks.
A blow bar takes high-speed strikes from whatever enters the chamber — including the occasional uncrushable. Edge toughness matters as much as hardness.
As the working edge rounds off the hit gets weaker: reduction ratio drops, oversize climbs and the recirculating load goes up.
Blow bars are replaced in sets for a reason. Uneven wear or mixed weights load the rotor bearings and shorten the life of everything else in the machine.
A chipped corner stops the bar being rotated onto its second face. If the bar cannot be turned, half of its service life is thrown away.
A blow bar change is a rotor-out job with a crane — and on a single-machine plant it stops the whole line.
A cheaper bar that chips early and cannot be rotated costs more per tonne crushed than an expensive bar that runs both faces.
Cost per campaign: a composite bar costs about 1.4× a plain manganese bar and returns roughly 2× the wear life once both faces are run. Against a carbide-bar composite of the same layout it lands at about 75% of the price.
| What happens at the edge | Effect on the rotor | Life from one bar |
|---|---|---|
| Wears evenly back | Bar is rotated, second face runs | Full — both faces used |
| Chips at a corner | Cannot be rotated safely | Half, thrown away |
| Cracks along the edge | Bar has to come out early | Shortened, unpredictably |
| Bars wear at different rates | Rotor goes out of balance | Shorter bearing and rotor life |
| Against a carbide bar composite of the same layout | Our bar lands at ≈ 75% of the price | |
Bars are weighed and supplied as a set, so the rotor goes back in balance whichever way the edge is running.
A blow bar is asked to do two opposite things at once: resist abrasion and absorb impact. Every grade is a different trade between the two. We cast all six — so the recommendation follows the rock, not the shelf.
An Al2O3 insert field cast into a high-chrome white-iron body. For silica, quartz and slag — no tramp metal.
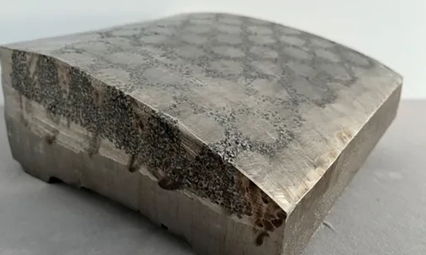
The same insert field on a martensitic body, so the bar bends where the high-chrome version chips. Mixed feed and mobile plants.
M7C3 white iron in a controlled section, then stress-relieved. HC-20 for granite and river gravel, HC-26 for quartzite.
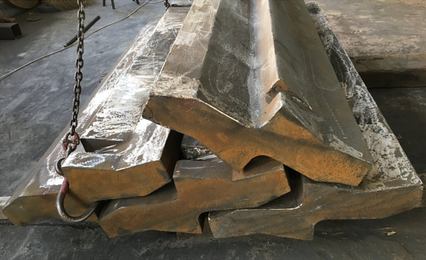
13% austenitic Mn that work-hardens under the hammer. The toughest of the six — recycling, C&D, and any chamber that eats tramp metal.
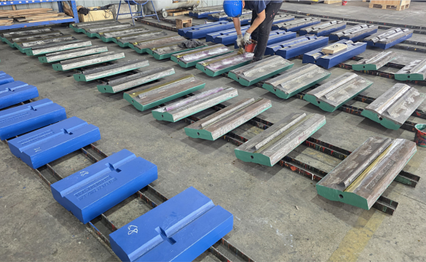
Cr-Mo steel, quenched and tempered. The mixed-feed default and the cheapest bar per tonne on soft, low-abrasion rock.
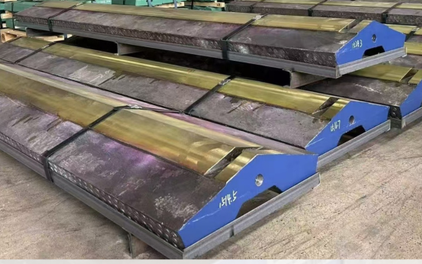
TiC rods cast into the wear face on our own line — a continuous field of rod ends, not glued-on tiles.
Abrasion picks the hardness, shock picks the toughness; when both are high the answer is a composite. Every quotation is priced per bar and per 10,000 t crushed.
| Feed material | Recommended | Runner up | Why |
|---|---|---|---|
| Limestone / dolomite | MS-45 | HC-20 | Low abrasion — toughness wins on cost per tonne |
| Construction & demolition | MS-45 | CER-MS | Tramp metal risk — a work-hardening body absorbs it |
| Granite / basalt | HC-20 | CER-HC | High abrasion, controlled top size |
| River gravel (rounded) | HC-20 | HC-26 | High abrasion with fines |
| Quartzite / silica sand | HC-26 | CER-HC | Very high abrasion, no tramp metal |
| Slag / mine waste | CER-HC / TiC | HC-26 | Abrasion plus shock — composite territory |
Same duty, same crusher, graded against the martensitic bar everyone starts with.
| Machine family | Bar types |
|---|---|
| Metso NP / Sandvik CI | Standard · Long · Heavy duty |
| Hazemag APK / APSE | Tooth · Smooth · Curved face |
| Kleemann MR / Terex Trakpactor | Standard · Long, mobile profiles |
| McCloskey RM / Striker / Gipo | Standard · Short · to sample |
| Any OEM, by sample | Sample → drawing → casting in 25–35 days |
Do not see your machine? Send the bar itself — sample to first casting runs 25–35 days.
Four things go into a price. Without all four the number is a guess, and guesses are what make a cheap bar expensive.
Model or worn-sample dimensions set the pattern.
Feed grading, abrasion index, tonnage per year.
One recommendation, one alternative, both priced.
Expected tonnes and cost per tonne, in writing.
What we need from you: the machine model, or the worn bar itself; feed grading and abrasion index; tonnage per year. What comes back: a wear section and hardness map, a written grade recommendation, and the price per bar and per 10,000 t.
Horizontal shaft impactors, stationary and mobile. These are the families we already tool patterns for — if yours is not listed, send the part number or a photo and we will confirm it.
Tell us the machine model and the part you are running now, and we will come back with the composite option measured against it.
A part number, a drawing, or a photo of the worn bar with the machine model is enough for us to identify the fitment. Tell us whether you rotate the bars, and we will lay the insert out for both faces.
How an order runs: confirm the bar and rotor position → check whether the bars are rotated → set the insert layout for both faces → 3D-print the pattern and machine the mould → cast, heat-treat, machine and weigh the set.
Send us your blow barAll manufacturer names, part numbers, model numbers and descriptions are used for identification and reference purposes only. It is not implied that any part listed is the product of the original manufacturer. Wear performance figures are laboratory values for the wear alloy itself and are not field-service guarantees. Patented in China (CN106282835B).